We do not just supply tools; we solve complex engineering problems, eliminate setups, improve CPK tolerances, and slash tooling expenses. Documented results validated by Tier-1 OEM recommendation letters.
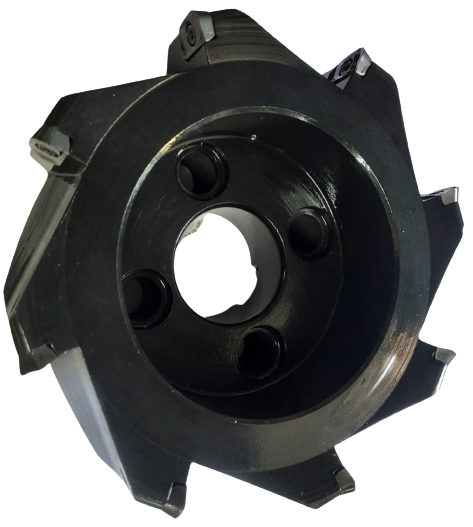 QTECH Multi-Operation Tooling
 Deming Award Win
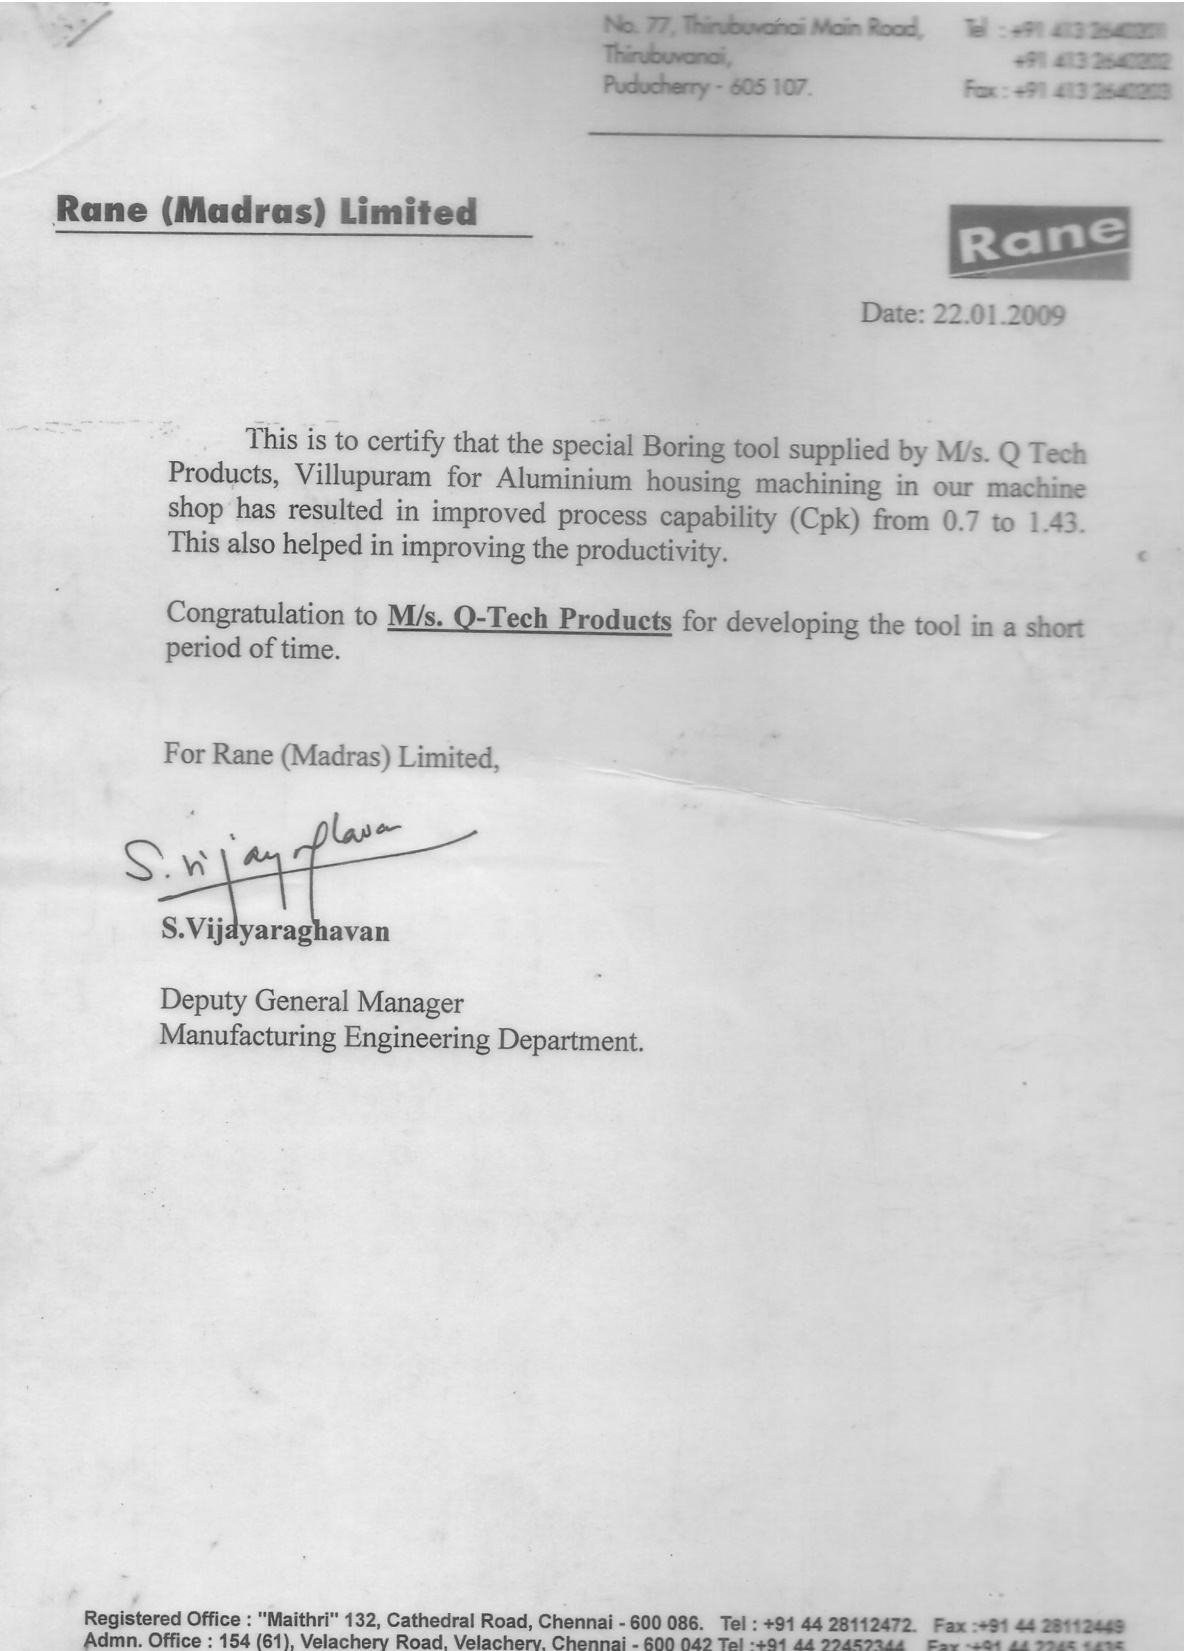
Rane (Madras) Ltd. machine shop in Puducherry was struggling with process capability on an aluminium steering housing bore: Ø12.99 mm with a tight 13-micron tolerance at a depth of 70 mm from the face. Tool deflection and chatter resulted in an unacceptable CPK of 0.70.
Within just one week, Q Tech Products engineered and manufactured a dedicated micro-fine boring bar featuring sub-micron radial adjustment and a tuned vibration-damping alloy shank.
"This solution improved process capability and supported Rane in securing the prestigious Deming Award." — S. Vijayaraghavan, Deputy General Manager, Manufacturing Engineering Department.
 Import Substitution
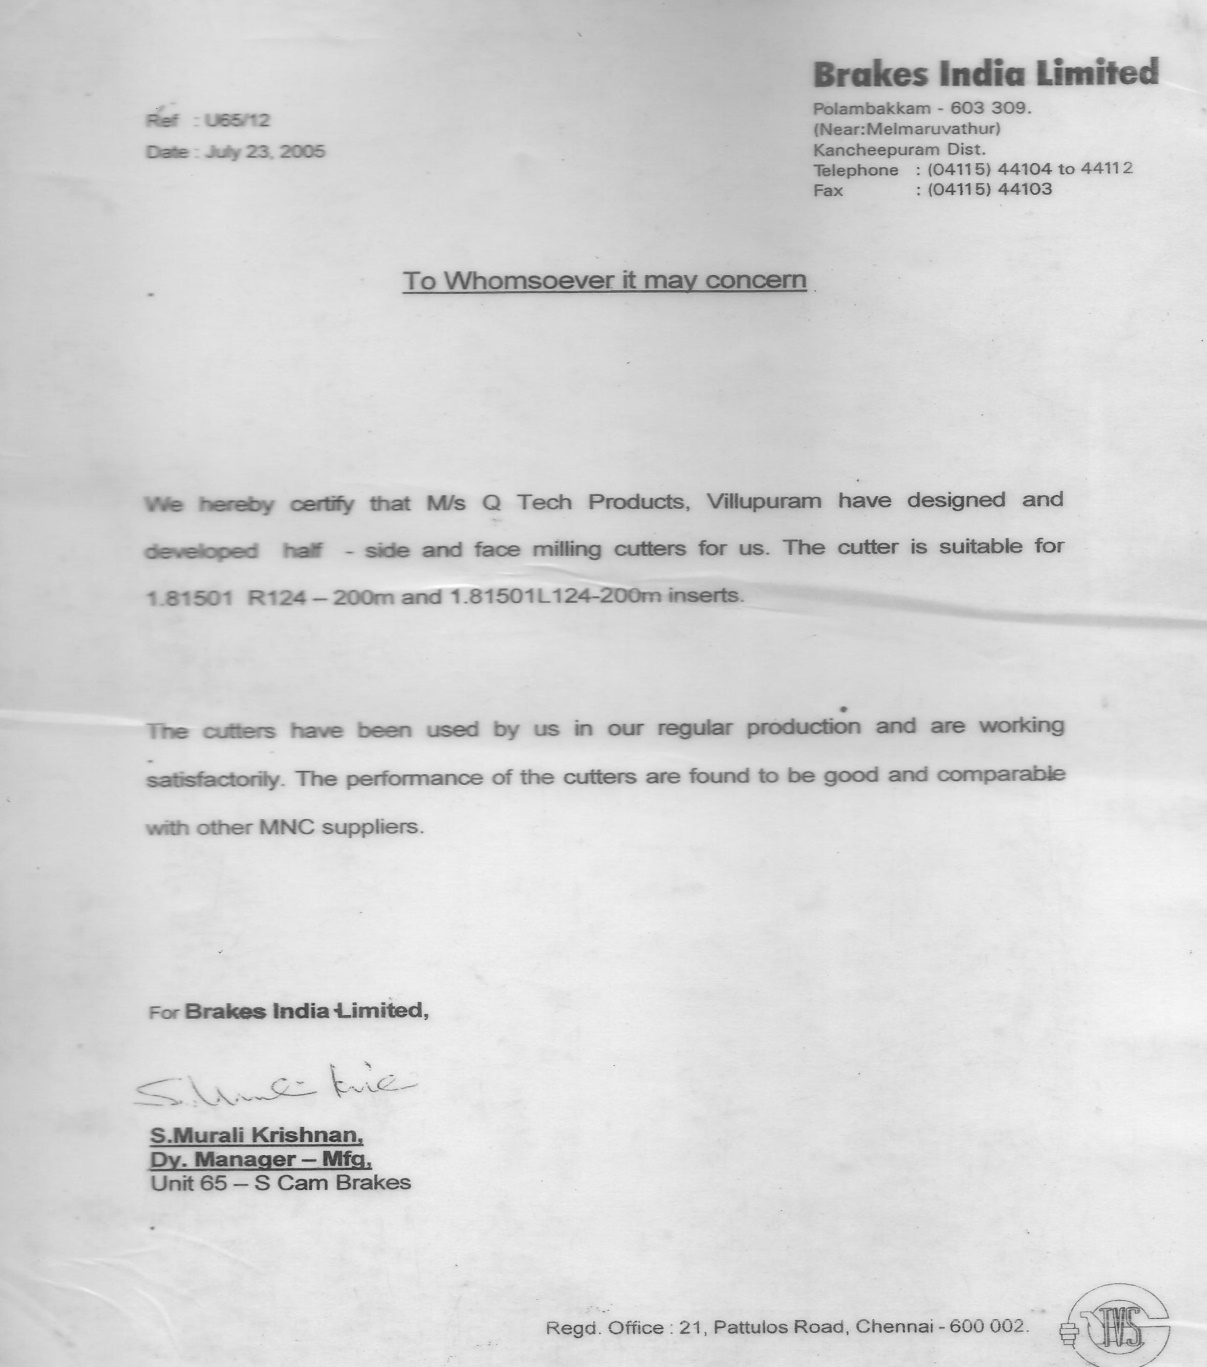
Brakes India Limited (Polambakkam Plant) depended on expensive imported European milling cutters for S-Cam brake manufacturing. When 2 or 3 insert pockets sustained damage, the entire expensive cutter body had to be scrapped, driving up tooling inventory costs.
Q Tech Products introduced an innovative modular cutter design where individual insert pockets are mounted as replaceable cartridges. If a pocket gets damaged, only the inexpensive cartridge is replaced in minutes. SECO inserts performed with equal or better tool life in the Q Tech cutter body.
"The performance of the cutters is found to be good and comparable with other MNC suppliers." — S. Murali Krishnan, Dy. Manager – Mfg, Unit 65 – S Cam Brakes, Brakes India Limited.
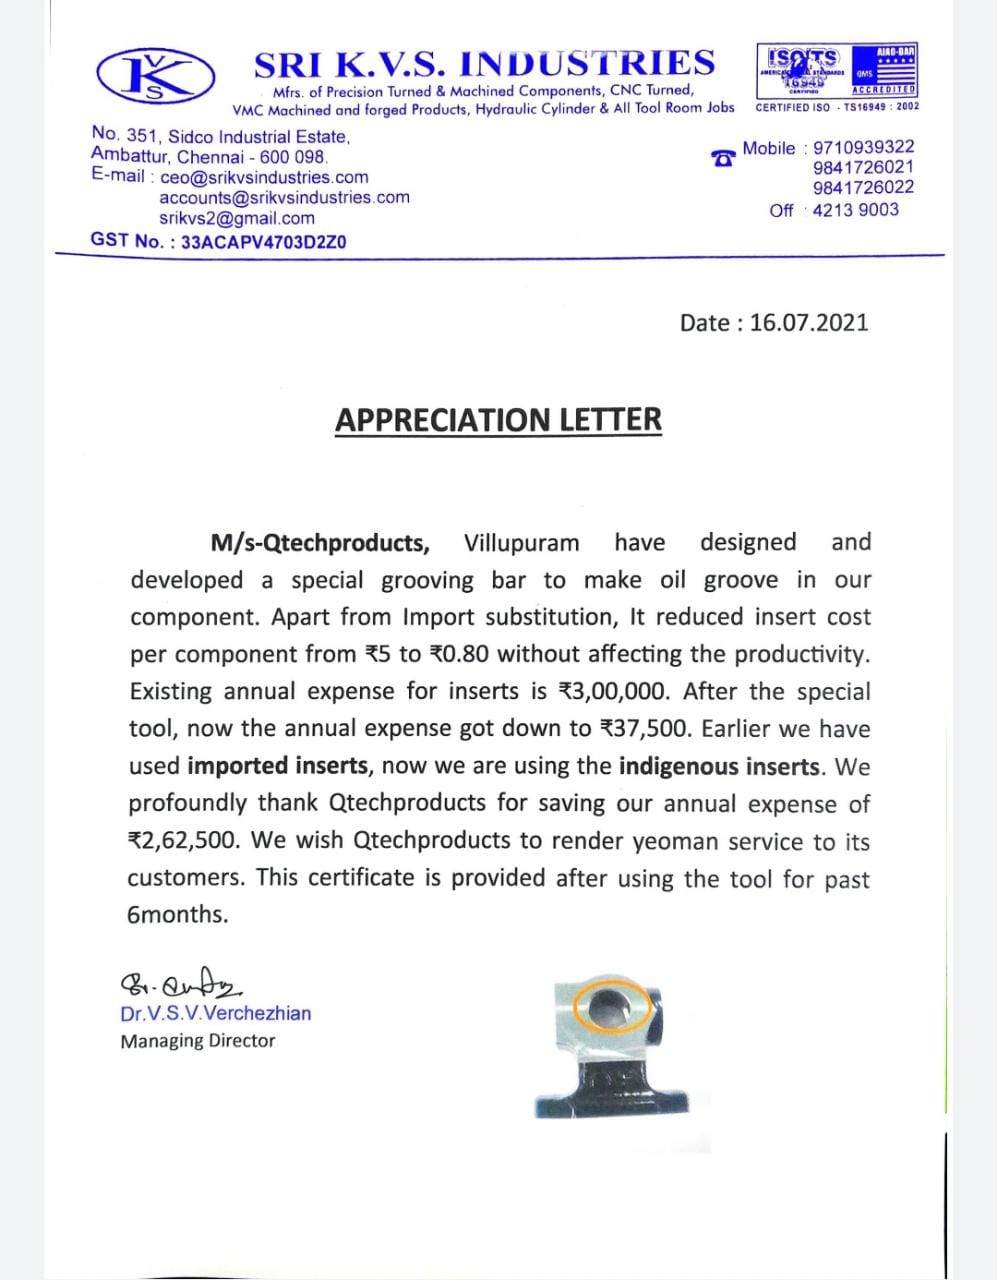
Sri KVS Industries (Ambattur Industrial Estate) was incurring ₹3,00,000 annually for specialized imported grooving inserts to machine oil grooves, paying ₹5.00 per component in consumable insert cost alone.
Q Tech Products re-engineered the grooving bar body to accept standard, universally available ISO turning inserts instead of costly proprietary inserts. Productivity and surface finish remained 100% identical.
"We profoundly thank Qtechproducts for saving our annual expense of ₹2,62,500. Earlier we used imported inserts, now we are using indigenous inserts." — Dr. V.S.V. Verchezhian, Managing Director.
Problem: Severe tool clearance and approachability constraints in tight motorcycle engine transmission pocket.
Solution: Engineered a compact high-clearance cartridge suitable for ISCAR inserts that reached the tight recess effortlessly without chatter.
 Burr Elimination
Problem: Heavy burr formation during PIP turning and reliance on costly zero corner radius inserts.
Solution: Custom twin-edged precision tool eliminated all burrs and allowed India Nippon to use economical standard 0.2/0.4 radius inserts across Hosur, Pondicherry, and Rewari plants.
 Single Setup
Problem: Two separate machines and two chucking setups required to finish rotor parts, causing concentricity deviations and high handling times.
Solution: Engineered a back-side turning tool operating in the same chucking setting, eliminating one entire machine setup and ensuring concentricity.