When standard catalog tools fail to meet your cycle time, tolerance, or approachability constraints, QTECH engineers bespoke indexable cutting tools built exclusively for your component drawing.
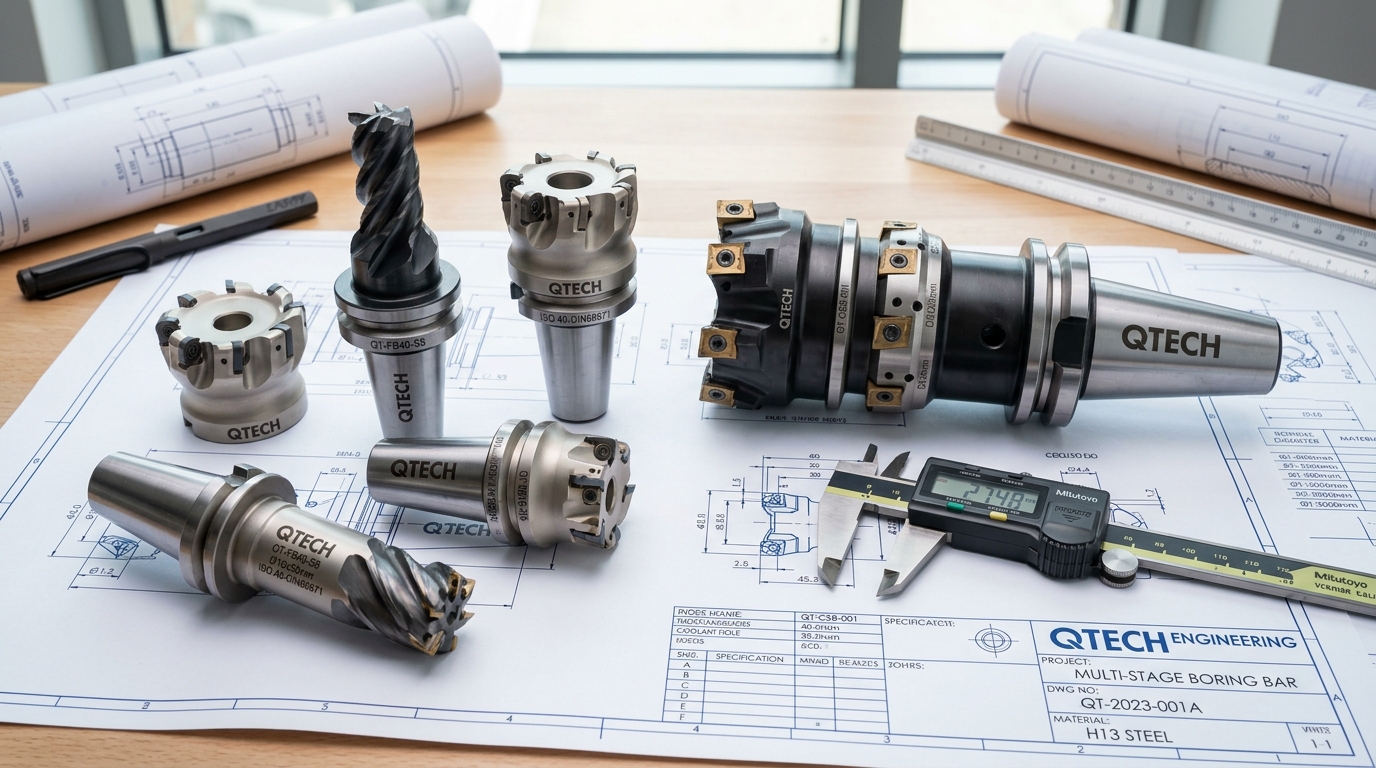 QTECH Custom Tooling & Drawings
In high-volume automotive and precision engineering production, using standard off-the-shelf tools often requires multiple machine passes, frequent tool changes, and costly proprietary inserts. When tolerances drop below 15 microns or deep bores introduce chatter, catalog tooling cannot adapt.
Q Tech Products approaches custom tooling as an engineering partnership. We examine the component drawing, analyze machine rigidity and spindle power, select standard ISO insert geometries to keep operating costs low, and engineer a rigid, balanced tool body tailored to the operation.
Every custom tool follows an audited, rigorous design and manufacturing workflow to guarantee zero trial-and-error on your production line.
Our engineers study your 2D/3D part drawings, workpiece material (hardness, cast iron, alloy steel, aluminum), cycle time targets, and machine interface (BT40, BT50, HSK, VDI).
Tool geometry, insert pockets, chip clearance flutes, and internal coolant circuits are designed in Solid Edge with 3D clearance simulations.
Toolpaths for 4-axis pocket milling and contouring are generated and verified to eliminate collisions and ensure pocket seating repeatability.
Manufactured on our LMW J1 VMC with rotary 4th axis from high-tensile alloy tool steel. Vacuum heat-treated to HRC 42–48 for core toughness.
100% inspection of pocket angles, insert seating, radial runout, and step lengths using Video Measuring Machine (VMM) and calibrated gauges.
On-machine tryout with your tooling engineers. Parameter optimization (cutting speed, feed, depth) to exceed CPK targets before handover.